ASTM B863 Grade 12 Titanium Wire
- Standard: ASTM B863
- Grade: Grade 12 (Ti-0.3Mo-0.8Ni Titanium Alloy)
- UNS: R53400
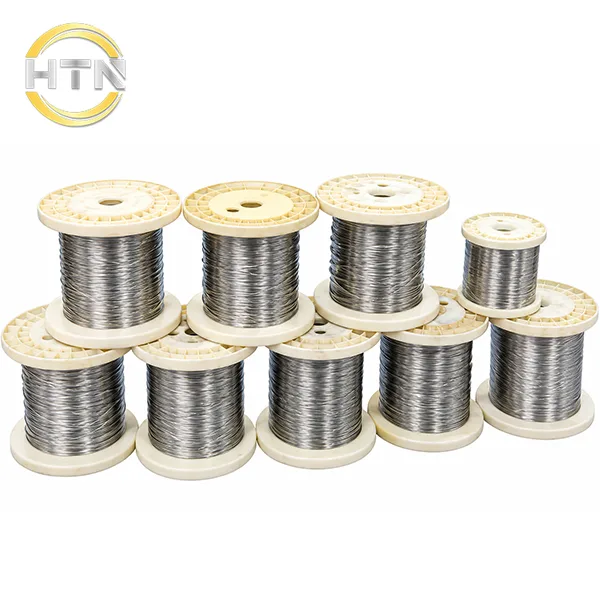
- Supply form: Coil, spool or straight cut length
- Condition: Annealed or cold-worked, as ordered
- Diameter Range: Ø0.03–Ø7.0 mm
Customizable sizes are available, while specific product parameters should be confirmed per the applicable standard edition and order.
Product Overview
ASTM B863 Grade 12 titanium wire is corrosion-resistant Ti-0.3Mo-0.8Ni alloy wire with UNS designation R53400. Small molybdenum and nickel additions raise strength and substantially improve the performance of unalloyed titanium in hot brines, crevices and some reducing media. Typical fields include chemical processing, desalination, hydrometallurgy, energy and marine equipment.
Grade 12 is generally stronger than Grade 2 while retaining good weldability and useful fabricability. Wire properties depend on diameter, cold reduction, annealed or stress-relieved condition, microstructure and surface quality. ASTM B863 Grade 12 wire does not automatically satisfy pressure-equipment, welding-consumable, medical-device or plant-design requirements.
| Specification | Details |
| Industrial Standard | ASTM B863 |
| Grades | Gr12 |
| Diameter Range | Ø0.03–Ø7.0 mm |
| Typical Diameters | Ø0.1, 0.2, 0.3, 0.4, 0.5, 0.6, 0.8, 1.0, 1.2, 1.5, 2.0, 2.5, 3.0, 4.0, 5.0, 6.0, 7.0 mm |
| Supply Form | Coil / Spool or straightened and cut wire |
Main Characteristics
- Balanced strength and corrosion resistance: Density is about 4.51 g/cm³ and a material-level minimum reference tensile strength is about 483 MPa, supporting thinner corrosion-resistant sections where design rules permit.
- Improved crevice-corrosion resistance over unalloyed titanium: Mo and Ni stabilize performance in hot brines, acidic chlorides and some mildly reducing conditions, particularly where Grade 2 may face crevice-corrosion risk.
- Good weldability: Qualified inert-gas fusion or resistance welding may be used; the pool, root and hot heat-affected zone must be protected from air and moisture contamination.
- Useful forming and drawing capability: Grade 12 can be drawn, coiled and formed, but its higher strength than Grade 2 requires validated tooling, lubrication, area reduction and intermediate annealing.
- Useful strength at moderate temperature: Service temperature, allowable stress and corrosion allowance must be established from the applicable design code and medium-specific data.
- Not directly equivalent to palladium-bearing grades: Grade 12 performs very well in many hot-brine and selected acidic services, but it is not Grade 7 or 11; medium, concentration, temperature, crevice and electrochemical conditions require individual evaluation.
Chemical Composition
The following limits apply to ASTM B863 Grade 12. Values are mass percentages. Formal acceptance is governed by the contract edition and the producer’s certified report.
| Element | ASTM B863 Grade 12 requirement |
| Molybdenum, Mo | 0.2-0.4% |
| Nickel, Ni | 0.6-0.9% |
| Nitrogen, N | ≤0.03% |
| Carbon, C | ≤0.08% |
| Hydrogen, H | ≤0.015% |
| Iron, Fe | ≤0.30% |
| Oxygen, O | ≤0.25% |
| Residual elements, each | ≤0.10% |
| Residual elements, total | ≤0.40% |
| Titanium, Ti | Balance |
Technical references: ASTM B863 grade scope and TIMETAL Grade 12 (Ti-0.8Ni-0.3Mo) technical data.
- Molybdenum and nickel: Mo supports beta stabilization, strength and resistance to reducing media; Ni works with Mo to improve performance in certain hot-brine and crevice conditions. Acceptance follows specified ranges, not only the nominal alloy name.
- Oxygen, iron and nitrogen: These elements affect strength, hardness, ductility and processing. Producer typical values must not replace ASTM maximum limits.
- Hydrogen: Must be strictly controlled. Improper pickling, cathodic protection or electrochemical exposure can promote hydrogen pickup, loss of ductility and hydride formation.
- Titanium content: ASTM states Titanium: Balance. A fixed titanium percentage calculated from nominal chemistry is not an untested product guarantee.
Mechanical Properties
ASTM B863 includes applicable tensile, elongation and hardness requirements for Grade 12 wire. Properties vary with diameter and delivery condition. Formal acceptance must follow the ordered condition, applicable size range, test method and official standard tables.
| Property | Product-page technical statement | Acceptance basis |
| Tensile strength | Depends on diameter and annealed/cold-worked condition | Applicable ASTM B863 table and purchase order |
| Elongation | Depends on diameter, gauge length and condition | Applicable ASTM B863 table and purchase order |
| Hardness | The specification includes applicable requirements; one value cannot cover every condition | Applicable grade, condition and test method |
| Yield strength | Minimum values defined for annealed condition(Rp0.2 ≥345 MPa); cold‑worked values vary with cold reduction & wire diameter, no universal fixed value | Specify condition, diameter and acceptance requirements in purchase order if yield strength is required |
Grade 12 Material Reference Properties (TIMETAL Grade 12 reference data, NOT ASTM B863‑26 wire guaranteed acceptance values)
| Property | TIMETAL Grade 12 material reference |
| Ultimate tensile strength | Minimum reference approx. 483 MPa |
| 0.2% yield strength | Minimum reference approx. 345 MPa |
| Elongation | Minimum reference approx. 18% |
| Reduction of area | Approx. 25% for bar/billet/forgings; not a wire guarantee |
Important: The values above are representative Grade 12 material data and are not universal ASTM B863 wire acceptance values. Diameter, cold reduction and final annealing affect strength, elongation and hardness. Quotations, contracts and MTRs should identify diameter, tolerance, condition, surface, coil weight or cut length, and inspection requirements.
HTN Supply and Quality Documentation
HTN organizes ASTM B863 Grade 12 Ti-0.3Mo-0.8Ni wire supply to customer purchase requirements. Material is produced by qualified titanium-mill resources. Original mill reports, heat traceability, full chemistry and property records can be supplied as agreed. HTN reviews the edition, heat number, diameter, tolerance, condition, surface, coil weight or cut length, and can arrange independent retesting, cut-to-length service, clean packaging and third-party inspection.
Typical Applications
- Corrosion-resistant wire parts for chemical heat exchangers, evaporators, condensers and reactors;
- mesh, support wire and connectors for desalination, salt processing and hot-brine systems;
- corrosion-resistant screens and filter elements for hydrometallurgy, mining and energy equipment;
- medium-strength fastening, tying or locating parts for marine and pollution-control equipment;
- precision corrosion-resistant wire parts requiring drawing, coiling, weaving, bending or flattening;
- critical parts only when additional pressure-equipment, design-code or customer requirements are satisfied;
- welding filler wire only when the applicable AWS A5.16 classification is met;
- special wire assemblies made to customer drawings and validated by corrosion, forming, fatigue or functional testing.
Application boundary: ASTM B863 Grade 12 wire is not automatically qualified pressure-equipment material, welding filler or permanently maintenance-free material for a specific corrosive service. Such uses separately require the applicable design code, AWS A5.16, customer drawing, corrosion data and quality-system requirements.
Fill in the form below and our team will be happy to assist you
Fabrication and Machining Characteristics
Drawing and Dimensional Control
Grade 12 is stronger than common unalloyed titanium. Drawing requires rigid equipment, clean tooling, suitable lubrication and controlled reduction, with intermediate annealing used to manage diameter, roundness, surface defects and residual stress.
Cold working
Cold working increases strength and hardness while reducing ductility. Final reduction, diameter and heat treatment must match subsequent coiling, weaving, bending, flattening or welding requirements.
Annealing and heat treatment
Annealing restores ductility, stabilizes microstructure and reduces residual stress. Time, temperature, atmosphere and cooling require a qualified procedure; generic temperatures are not purchase guarantees.
Welding and joining
GTAW/TIG, laser welding, resistance welding or another qualified method may be used with complete inert-gas shielding of the pool, root and hot heat-affected zone. Filler wire must separately satisfy the applicable AWS A5.16 classification, consumable chemistry, cleanliness, dimensions and procedure qualification; ASTM B863 compliance alone does not qualify welding wire.
Typical Physical Properties
The following are representative TIMETAL Grade 12 values near room temperature and are not mandatory lot-acceptance requirements of ASTM B863 .
| Physical property | Typical value |
| Density | Approx. 4.51 g/cm³ |
| Tensile modulus at room temperature | Approx. 103 GPa |
| Shear modulus at room temperature | Approx. 42.7 GPa |
| Thermal conductivity at 24°C | Approx. 19.0 W/(m·K) |
| Electrical resistivity at 24°C | Approx. 0.52 μΩ·m |
| Coefficient of thermal expansion near 24°C | Approx. 9.54×10⁻⁶/K |
| Specific heat at 24°C | Approx. 0.544 kJ/(kg·K) |
| Magnetism | Essentially non-magnetic |
| Beta transus | Varies with chemistry and microstructure; test when ordered |
Physical-property reference: TIMETAL Grade 12 technical data. Values vary with heat, temperature, microstructure, cold work and heat-treatment condition.
Corrosion Resistance
Grade 12 obtains excellent corrosion resistance from the stable titanium-oxide film and beneficial Mo-Ni additions. Compared with Grade 2, it commonly provides a wider operating window in hot brines, crevices and some acidic or mildly reducing media, but it is not immune to all chemical environments.
Environments in Which Grade 12 Generally Performs Well or Merits Priority Evaluation
- Seawater, brine, salt spray and humid air;
- hot brines and chloride systems containing crevices;
- many oxidizing acids and oxidizer-containing process streams;
- selected mildly reducing acids and organic-acid services;
- desalination, salt-processing and high-purity-water systems;
- wet chlorine and hydrated halogen environments;
- selected hydrometallurgical and mineral-processing media;
- validated chemical heat-transfer, condensation and evaporation services.
Environments Requiring Careful Evaluation
- Fluoride-containing media or hydrofluoric acid;
- concentrated strong reducing acids under oxygen-starved conditions;
- anhydrous methanol or halide-contaminated methanol;
- red fuming nitric acid;
- molten chloride salts and extreme high-temperature salt service;
- cathodic-protection or electrochemical conditions that may promote hydrogen absorption;
- unknown combinations of high stress, deposits and very tight crevices;
- dissimilar-metal contact with an unsuitable galvanic design;
- any service lacking reliable temperature, concentration, velocity and contaminant data.
Engineering caution: Grade 12 is not immune to every corrosive environment. Fine wire, mesh and woven structures may also be affected by crevices, deposits, contacting metals and cleaning residues. Hot chlorides, strong reducing acids, fluoride media and electrochemical conditions require specific evaluation.
Typical Industry Manufacturing Route for Grade 12 Titanium Wire
- Raw-material selection and charge preparation: Select qualified titanium sponge, molybdenum-nickel alloy additions and controlled clean revert, accurately controlling Mo, Ni, O, Fe, N and H.
- Electrode preparation: Homogenize, compact and weld a consumable electrode while avoiding Mo-Ni segregation and contamination from iron particles, oil and moisture.
- Vacuum melting and ingot production: VAR or another qualified vacuum route is commonly used for chemistry uniformity and cleanliness. ASTM B863 does not prescribe one identical melt count for every Grade 12 wire order; special requirements belong in the purchase order.
- Ingot conditioning and breakdown: Crop unsuitable ends, remove surface defects, and forge or roll to produce billet or rod suitable for wire processing.
- Hot processing to wire rod: Forge, hot roll or make coil in a controlled range, managing microstructure, dimensions, oxidation and surface quality.
- Surface conditioning and multi-pass drawing: Remove scale and alpha case, condition laps or cracks, and draw through successive dies with intermediate anneals scheduled to accumulated reduction.
- Intermediate and final heat treatment: Apply a qualified anneal or agreed condition, controlling time, temperature, atmosphere and cooling to obtain specified properties.
- Surface finishing: Use pickling, mechanical cleaning, polishing or another approved method while controlling hydrogen pickup, oxidation, iron contamination and surface notches.
- Straightening, coiling and cutting: Supply on coils or spools, or as straight cut lengths, and inspect diameter, roundness, straightness, coil quality and surface condition.
- Inspection and traceability: Verify chemistry, tensile properties, elongation, hardness, dimensions and surface quality, maintaining traceability from heat and lot to package and material-test documentation.
Melting and inspection note: ASTM B863 requires finished wire to meet applicable chemistry, performance, dimensional and quality requirements. It does not prescribe the same number of VAR melts for every Grade 12 product. Double or triple VAR, tight roundness, special roughness, cleanliness, nondestructive testing, EN 10204 3.1 documentation and third-party inspection must be confirmed in the purchase order when required.