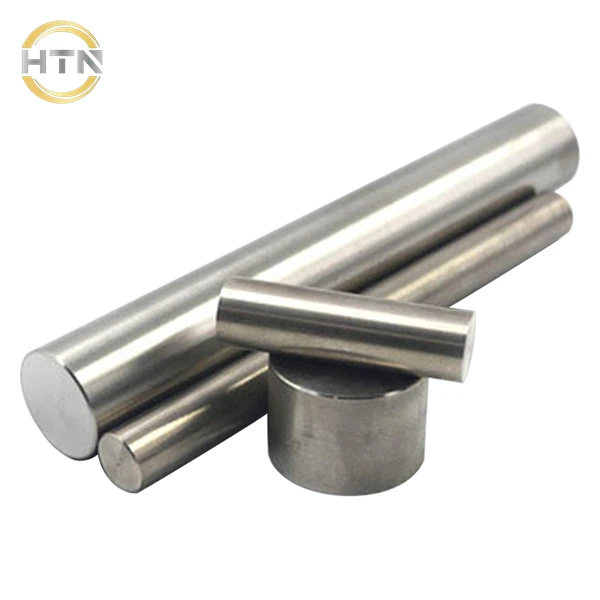
ASTM B348 Grade 23 Titanium Rod / Bar
- Standard: ASTM B348
- Grade: Grade 23
- Material type: Ti-6Al-4V ELI extra-low-interstitial alpha-beta titanium alloy
- UNS: R56407
- Room-temperature structure: Typical alpha-beta microstructure
- Condition: Annealed
- Dia: φ7 ~ φ300 mm
- Typical Industrial Bar Length: 200–3000 mm
Customizable sizes are available, while specific product parameters should be confirmed per the applicable standard edition and order.
Product Overview
ASTM B348 Grade 23 titanium rod/bar is a Ti-6Al-4V ELI (Extra Low Interstitial) alpha-beta titanium alloy bar produced and tested to ASTM B348/B348M. The alloy is UNS R56407, with 5.50% to 6.50% aluminum and 3.50% to 4.50% vanadium, together with tighter limits on oxygen, iron and hydrogen than Grade 5.
Grade 23 is the low-interstitial variant of Grade 5 (Ti-6Al-4V). Its lower oxygen, iron and hydrogen limits support improved ductility and fracture toughness, making it appropriate for critical applications requiring material cleanliness, damage tolerance, fatigue performance and heat traceability. It is commonly supplied annealed; final strength, microstructure and testing must be confirmed against the applicable specification, dimensions and purchase requirements.
Grade 23 bar is suitable for medical-device and implant machining stock when ASTM F136 or a customer medical specification is separately ordered and accepted, as well as aerospace fasteners and structures, marine and energy hardware, high-performance sporting equipment, scientific instruments and other precision components requiring high specific strength, corrosion resistance and toughness.
| Specification | Details |
| Industrial Standard | ASTM B348 |
| Industrial Grades | Gr23 |
| Diameter Range | Ø7 – Ø300 mm |
| Typical Diameters | Ø7, 8, 10, 12, 14, 16, 18, 20, 25, 30, 35, 40, 45, 50, 60, 70, 80, 90, 100, 120, 150, 200 mm |
| Typical Industrial Bar Length | 200–3000 mm; cut-to-length available |
| Surface / Supply Condition | Hot-rolled black surface / Turned / Ground |
| Precision Tolerance | h6 / h7 / h8 available subject to diameter, finishing process and order confirmation |
Main Characteristics
- Lower interstitial-element content: Oxygen is limited to 0.13%, iron to 0.25% and hydrogen to 0.0125%. Compared with Grade 5, this control generally supports better ductility and fracture toughness; actual performance depends on microstructure, heat treatment, section size and test direction.
- High strength: Annealed ASTM B348 Grade 23 minimum tensile strength is 828 MPa, minimum 0.2% offset yield strength is 759 MPa, minimum elongation is 10% and minimum reduction of area is 25%.
- Good corrosion resistance: A stable titanium-oxide passive film gives good performance in many oxidizing and chloride-bearing aqueous environments. Grade selection must still be based on medium, temperature, concentration, oxygen availability and crevice conditions.
- Good weldability: TIG, electron-beam, laser and other qualified processes may be used. The joint must be clean and the weld pool, face, root and hot heat-affected zone require complete high-purity inert-gas shielding.
- Heat-treatment flexibility: Annealing, stress relief or solution treatment and aging may be used under qualified procedures to adjust strength, ductility and microstructure. The thermal condition, final supply condition and required properties must be stated in the order.
- Medical use requires separate confirmation: ASTM B348 Grade 23 is not automatically equivalent to ASTM F136 implant-grade material. For implants or medical devices, the order must state the ASTM F136 edition and any required chemistry, microstructure, surface, cleanliness, documentation and supplementary controls.
Chemical Composition
ASTM B348 Grade 23 chemistry is controlled to the following mass-percent limits:
| Element | ASTM B348 Grade 23 requirement |
| Nitrogen, N | ≤0.030% |
| Carbon, C | ≤0.080% |
| Hydrogen, H | ≤0.0125% |
| Iron, Fe | ≤0.250% |
| Oxygen, O | ≤0.130% |
| Aluminum, Al | 5.50%–6.50% |
| Vanadium, V | 3.50%–4.50% |
| Residual elements, each | ≤0.100% |
| Residual elements, total | ≤0.400% |
- Aluminum and vanadium are the principal alloying elements in Ti-6Al-4V ELI, supporting an alpha-beta microstructure and high strength. Their levels, together with thermomechanical processing and heat treatment, affect strength, toughness and microstructure.
- Oxygen, nitrogen, carbon, hydrogen and iron require close control. The lower oxygen, iron and hydrogen limits distinguish Grade 23 from Grade 5; excessive oxygen and iron can reduce toughness, while excessive hydrogen can form brittle hydrides.
- Final chemistry shall be confirmed by the original mill test report for the applicable heat. ASTM F136 for medical use, aerospace specifications, customer drawings and any more-stringent requirements must be stated in the order and shall not be inferred from ASTM B348 documentation alone.
Mechanical Requirements
The following room-temperature tensile requirements apply to annealed ASTM B348 Grade 23 bar. The specified edition, dimensions, specimen form, test orientation and supplementary requirements must also be considered for formal acceptance.
| Property | Requirement | Status |
| Ultimate tensile strength, Rm | ≥828 MPa | ASTM minimum |
| 0.2% offset yield strength, Rp0.2 | ≥759 MPa | ASTM minimum |
| Elongation in the specified gauge length | ≥10% | ASTM minimum |
| Reduction of area, Z | ≥25% | ASTM minimum |
Typical room-temperature properties (not guaranteed)
| Property | Reference Value |
| Ultimate tensile strength | Approx. 860–965 MPa |
| 0.2% offset yield strength | Approx. 795–895 MPa |
| Elongation | Approx. 10–18% |
| Reduction of area | Approx. 25–40% |
| Elastic modulus | Approx. 107–122 GPa |
Important: Typical values are not ASTM acceptance values and are not automatically guaranteed for every lot. Hardness, UT, PMI, microstructure, fatigue, fracture toughness, ASTM F136, medical cleanliness or other tests must be ordered when required.
HTN Supply and Quality Services
ASTM B348 Grade 23 titanium bar is produced by evaluated, qualified mill resources. HTN confirms technical requirements from customer drawings and purchase specifications, selects a mill with appropriate capability, reviews the original MTR and heat/lot records, and verifies the relationship among material standard, dimensions, quantity, condition and inspection documents.
When agreed in the contract, HTN can coordinate independent retesting, ultrasonic examination, PMI, microstructure examination, cut-to-length service, turning or grinding, EN 10204 3.1 documentation and third-party inspection, together with export packing, shipping documents and international delivery.
Typical Applications
- Medical-device and implant machining stock, when ASTM F136 or customer medical requirements are separately confirmed;
- aerospace fasteners, structures, engine parts and other high-performance machined components;
- marine engineering, shipboard, energy, instrumentation and high-performance sporting-equipment components;
- pump and valve hardware, flanges, pressure-equipment parts and custom components requiring high specific strength and corrosion resistance;
- research equipment, precision instruments and engineering uses requiring material cleanliness, strength, toughness and traceability;
- other critical uses evaluated against drawings, standards, supply condition and service environment.
Fill in the form below and our team will be happy to assist you
Fabrication and Processing Characteristics
Machining
Grade 23 can be turned, milled, drilled, ground and threaded. Its low thermal conductivity, elastic recovery and tendency to gall call for sharp, rigid tooling, stable feed, appropriate cutting speed and abundant non-chlorinated cutting fluid. Tool dwell, rubbing and localized overheating should be avoided.
Cold forming
Its room-temperature cold-forming latitude is lower than that of commercially pure titanium. Complex or tight-radius shapes should be validated by trial or qualified procedure, using staged forming, intermediate annealing or warm forming when needed to control springback, surface damage and cracking risk.
Hot working and heat treatment
Bar can be produced through vacuum melting, forging, hot rolling, extrusion, drawing and finishing. Working temperature, reduction, soak time, cooling path and atmosphere must follow a qualified process to obtain the required alpha-beta microstructure and limit grain coarsening, oxidation and alpha case. Annealing, stress relief or solution treatment and aging shall follow the order and applicable specification.
Welding
Grade 23 has good weldability but is sensitive to contamination. The weld pool, face, root and hot heat-affected zone require complete high-purity inert-gas shielding. Critical weldments should be qualified for joint strength, ductility, fatigue performance, corrosion behavior and any required post-weld treatment.
Machining safety: Fine titanium chips and powders are combustible and must be collected, stored and handled away from ignition sources under applicable safety requirements.
Typical Physical Properties
The following are typical reference values near room temperature and are not mandatory lot-acceptance requirements of ASTM B348:
| Physical property | Typical value |
| Density | Approx. 4.42 g/cm³ |
| Elastic modulus | Approx. 107–122 GPa |
| Specific heat at room temperature | Approx. 0.580 J/(g·K) (at 20°C) |
| Thermal conductivity | Approx. 6.6 W/(m·K) (at 20°C) |
| Electrical resistivity | Approx. 1.68 μΩ·m (at 0°C) |
| Mean CTE, 0–100°C | Approx. 9.0×10⁻⁶/K |
| Beta transus | Approx. 995°C |
| Melting temperature | Approx. 1650–1660°C |
| Poisson’s ratio | Approx. 0.31 |
| Magnetism | Generally regarded as non-magnetic |
Physical-property reference: TIMET public Ti-6Al-4V / Ti-6Al-4V ELI technical data. Values vary with temperature, heat, microstructure, orientation, section size and heat-treatment condition.
Corrosion Resistance
Grade 23 corrosion resistance is based on a continuous, tightly adherent titanium-oxide passive film. It performs well in many oxidizing media, seawater and chloride-bearing aqueous environments. Compared with commercially pure titanium, Ti-6Al-4V ELI must not be selected by grade alone; reducing acids, oxygen-starved crevices, hot brines and fluoride-bearing media require engineering evaluation against actual medium, temperature, concentration, flow, stress and crevice conditions.
Environments in Which Grade 23 Generally Performs Well
- Natural seawater, marine atmospheres, salt spray and many chloride-bearing aqueous media;
- many neutral aqueous solutions, general industrial water, desalination and applicable heat-transfer service;
- nitric acid and many other oxidizing acidic environments;
- evaluated chemical-processing, marine, energy, aerospace and medical-device related service environments;
- custom engineering parts requiring high specific strength, corrosion resistance and material cleanliness.
Environments Requiring Careful Evaluation
- Fluoride-bearing media or hydrofluoric acid;
- hot, concentrated, oxygen-starved or strongly corrosive acids containing reducing metal ions;
- completely dry chlorine, anhydrous methanol or halide-contaminated methanol;
- red fuming nitric acid, molten chloride salts, liquid mercury, cadmium and other special chemical environments;
- pickling, cathodic protection or electrochemical conditions that may promote hydrogen pickup, as well as hot crevices, deposits, dissimilar-metal contact and stressed locations.
- hot crevices, deposits, dissimilar-metal contact and stressed locations.
Engineering caution: Grade 23 corrosion resistance cannot be determined by alloy grade alone. Fluoride-bearing media, reducing acids, oxygen-starved crevices and hot brines require actual-service corrosion testing and engineering review.
Typical Industry Manufacturing Route for Grade 23 Titanium Rod
- Raw-material and charge preparation: Select qualified titanium sponge, aluminum-vanadium master alloy and approved clean revert, while closely controlling oxygen, nitrogen, carbon, hydrogen, iron and foreign contamination.
- Electrode preparation: Compact the charge into electrode blocks and assemble the melting electrode, ensuring uniform aluminum and vanadium distribution and exclusion of oil, moisture and iron-bearing foreign matter.
- Vacuum melting and ingot production: Multiple VAR melts are commonly used; electron-beam cold-hearth melting or another approved titanium melting route may also be used. The melting route and number of melts follow the qualified mill process and purchase requirements.
- Ingot conditioning and chemistry: Crop, peel or grind as necessary, complete required chemical analysis, retain heat identification and perform necessary internal-quality controls.
- Breakdown forging: Upset, draw or multi-directionally forge to break down the cast structure, improve internal uniformity and produce billet for further working.
- Alpha-beta hot working and bar formation: Forge, hot roll, extrude, draw or combine processes to produce the required section, controlling temperature, reduction and cooling path for a stable alpha-beta microstructure.
- Heat treatment: Anneal, stress-relief anneal or, when ordered, solution treat and age under a qualified procedure to obtain the required strength-ductility balance and microstructure.
- Surface conditioning, straightening and finishing: Turn, grind, blast, pickle, straighten, cut, chamfer or polish as required. Pickling must limit hydrogen pickup and meet surface-quality requirements.
- Final inspection, documentation and delivery: Verify chemistry, tensile properties, dimensions, tolerances, surface and identification. UT, PMI, microstructure, hardness, fatigue, fracture-toughness, medical supplementary testing or third-party inspection are performed when ordered. Maintain full correlation among material, labels, heat, lot, condition and original MTR.