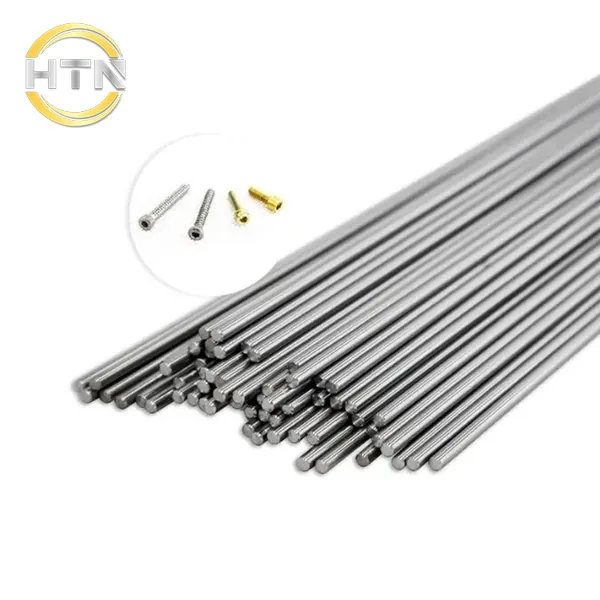
ASTM F67 Grade 3 Unalloyed Titanium Bar
- Standard: ASTM F67
- Grade: Grade 3 (Unalloyed Titanium)
- UNS: R50550
- Supply form: Round bar or other ordered bar form
- Condition: Annealed, as ordered
- Dia: φ7 ~ φ300 mm
- Typical Medical Bar Length: 2000–3000 mm; cut-to-length available
Customizable sizes are available, while specific product parameters should be confirmed per the applicable standard edition and order.
Product Overview
ASTM F67 Grade 3 unalloyed titanium bar is wrought commercially pure titanium bar used to manufacture surgical implants, UNS R50550. Among the four unalloyed grades in ASTM F67, Grade 3 provides relatively high strength while retaining useful ductility, corrosion resistance and fabricability. Its performance is achieved principally through a higher but controlled oxygen level together with limits on iron, nitrogen, carbon and hydrogen.
The material offers good biocompatibility, resistance to physiological corrosion and higher strength for medical-device raw material requiring greater strength than Grade 2 with moderate forming complexity. ASTM F67 compliance applies to the raw material; it does not mean a finished implant has completed design verification, biological evaluation, cleaning, sterilization or regulatory approval.
| Specification | Details |
| Industrial Standard | ASTM F67 |
| Industrial Grades | Gr3 |
| Diameter Range | Ø7 – Ø300 mm |
| Typical Diameters | Ø7, 8, 10, 12, 14, 16, 18, 20, 25, 30, 35, 40, 45, 50, 60, 70, 80, 90, 100, 120, 150, 200 mm |
| Typical Medical Bar Length | 2000–3000 mm; cut-to-length available |
| Surface / Supply Condition | Hot-rolled black surface / Turned / Ground |
| Precision Tolerance | h6 / h7 / h8 available subject to diameter, finishing process and order confirmation |
Medical-use boundary: ASTM F67-compliant bar is medical-device raw material, not an approved finished implant. The device manufacturer remains responsible for design, manufacturing, cleaning, sterilization, biological evaluation, risk management and regulatory compliance.
Main Characteristics
- Higher strength: Annealed Grade 3 is stronger than Grades 1 and 2 and is suited to unalloyed titanium parts requiring greater load capacity and resistance to deformation.
- Controlled unalloyed chemistry: No nominal alloying addition is made; O, Fe, N, C and H are controlled to provide higher strength while retaining useful ductility, toughness and processing consistency.
- Good biocompatibility: A stable TiO2 passive film helps limit ion release in physiological environments. The finished device still requires applicable biological evaluation.
- Good corrosion resistance: Performance is generally excellent in saline, body fluids and many chlorides, but crevices, fretting corrosion, dissimilar-metal coupling and fluoride exposure require device-level evaluation.
- Good weldability: Qualified inert-gas, laser or resistance welding may be used; hot metal must be protected from O, N, H and C contamination.
- Lower forming margin than lower grades: Grade 3 has higher strength, but ductility and cold-forming margin are generally lower than Grades 1 and 2. Load-bearing implants still require design verification using actual load, fatigue, geometry, surface condition and service-life requirements.
Chemical Composition
The following limits apply to ASTM F67 Grade 3. Values are mass percentages. Formal acceptance is governed by the contract edition and producer certified report.
| Element | ASTM F67 Grade 3 requirement |
| Nitrogen, N | ≤0.05% |
| Carbon, C | ≤0.08% |
| Hydrogen, H | ≤0.015% |
| Iron, Fe | ≤0.30% |
| Oxygen, O | ≤0.35% |
| Residual elements, each | ≤0.10% |
| Residual elements, total | ≤0.40% |
| Titanium, Ti | Balance |
Technical references: ASTM F67 official scope and producer data for Grade 3 / UNS R50550.
- Oxygen, nitrogen and iron: Oxygen is the principal interstitial strengthener used to obtain Grade 3 strength; nitrogen and iron also contribute. Grade 3 permits higher oxygen and nitrogen limits than Grade 2, increasing strength while reducing ductility and complex-forming capability.
- Nitrogen, carbon and hydrogen: These elements require strict control. Excess content raises hardness and reduces ductility; hydrogen may promote hydrides and embrittlement.
- Residual elements: Each and total limits must be controlled. Testing only the principal impurities does not satisfy the full chemistry requirement.
- Titanium content: The specification states Titanium: Balance. A nominal purity claim does not replace heat-specific chemical analysis and the material report.
Mechanical Properties
ASTM F67 specifies room-temperature tensile properties for Grade 3 wrought products. Bar acceptance must follow the applicable size, sampling position and direction, specimen form, condition and official standard table.
| Property | ASTM F67 Grade 3 annealed reference | Note |
| Ultimate tensile strength | ≥450 MPa | Official applicable product table governs |
| 0.2% yield strength | 380-550 MPa | A specified range, not one minimum |
| Elongation | ≥18% | Subject to size and specimen conditions |
| Reduction of area | Per applicable product/specimen requirement | Check official table when ordered |
ASTM F67 Grade 3 Annealed Bar Reference Requirements
| Property | Grade 3 annealed reference |
| Ultimate tensile strength | Minimum 450 MPa |
| 0.2% yield strength | 380-550 MPa |
| Elongation | Minimum 18% |
| Elastic modulus | Typical approx. 105 GPa |
Important: Mechanical properties must be applied with bar size, sampling location and direction, specimen form and the official table. Generic website data cannot replace contract acceptance, and ASTM F67 raw-material compliance alone does not qualify a finished implant.
HTN Supply and Quality Documentation
HTN organizes ASTM F67 Grade 3 unalloyed titanium bar supply to customer purchase requirements. Material is produced by qualified titanium-mill resources. Original mill reports, heat traceability, chemistry and mechanical records can be supplied as agreed. HTN reviews edition, heat number, diameter, tolerance, condition, surface, straightness and packaging, and can arrange independent retesting, ultrasonic testing, cutting, clean packaging and third-party inspection.
Typical Applications
- Machining stock for orthopedic, trauma or cranio-maxillofacial fixation parts after device-level validation;
- machining stock for dental instruments, abutments, restorative components and higher-strength precision connectors;
- surgical-instrument parts requiring relatively high strength, good corrosion resistance and moderate ductility;
- raw material for implant components, supports, fasteners and structural unalloyed titanium parts;
- medical fastening, connecting, locating and support parts;
- precision bar parts manufactured to customer drawings;
- research, prototype and custom medical-device material;
- international projects when ISO 5832-2, regulatory and customer requirements are also met.
Application boundary: ASTM F67 Grade 3 bar is raw material for surgical implant applications, not an approved finished implant. The final device must separately meet applicable regulations, design validation, biological evaluation, cleaning, sterilization and traceability requirements.
Fill in the form below and our team will be happy to assist you
Fabrication and Machining Characteristics
Hot Processing, Finishing and Dimensional Control
Grade 3 bar may be formed by forging, rolling, hot drawing or another qualified method, then turned, peeled, centerless ground or polished to the ordered dimensions and surface condition. Subsequent machining still exhibits titanium's low thermal conductivity, tool adhesion and elastic recovery; use sharp tools, rigid setups, positive rake, ample coolant and controlled continuous feed to avoid surface damage and work hardening.
Cold working and forming
Grade 3 may be bent, flattened, reduced or end formed under controlled conditions, but its forming margin is lower than Grades 1 and 2. Larger bend radii and intermediate annealing may be required. Actual limits depend on diameter, grain size, surface defects, working direction and cold-work level.
Annealing and heat treatment
Annealing restores ductility, lowers residual stress and stabilizes equiaxed alpha microstructure. Unalloyed titanium is not conventionally precipitation hardened; Grade 3 obtains its higher strength mainly from controlled interstitial elements, and cold work can further increase strength. Qualified atmospheres are required to prevent oxidation and alpha case.
Welding and joining
Qualified GTAW/TIG, laser or resistance welding may be used. Clean thoroughly before welding and fully shield the pool, root and hot heat-affected zone. Device welds require strength, fatigue, corrosion and cleanliness validation.
Typical Physical Properties
The following are typical Grade 3 values near room temperature; unless explicitly specified, they are not mandatory lot-acceptance values of ASTM F67 .
| Physical property | Reference value |
| Density | Approx. 4.51 g/cm³ |
| Elastic modulus at room temperature | Approx. 105 GPa |
| Thermal conductivity at 21°C | Approx. 16 W/(m·K) |
| Mean CTE, 20-100°C | Approx. 8.6×10⁻⁶/K |
| Melting temperature reference | Approx. 1670°C |
| Poisson’s ratio | Typically approx. 0.34 |
| Crystal structure at room temperature | HCP alpha titanium |
| Magnetism | Essentially non-magnetic |
| Strengthening mechanism | Mainly cold work; not conventionally age hardenable |
| Specific heat at room temperature | Typically approx. 520 J/(kg·K) |
Physical-property reference: Producer data for Grade 3 / UNS R50550. Values vary with temperature, microstructure, orientation, cold work and heat treatment.
Corrosion Resistance
Grade 3 develops a spontaneous, renewable TiO2 passive film and generally resists saline, body fluids and many chloride environments. Actual device performance also depends on surface treatment, crevices, micromotion, dissimilar metals, electrochemical conditions and sterilization or cleaning residues.
Environments in Which Grade 3 Generally Performs Well
- Saline and many simulated-body-fluid environments;
- humid air and high-purity water;
- neutral chloride solutions;
- many oxidizing environments;
- properly controlled cleaning and passivation processes;
- many medical-device sterilization processes after device validation;
- long-term tissue contact without fretting;
- validated dental and orthopedic device environments.
Environments Requiring Careful Evaluation
- Fluoride cleaners, hydrofluoric acid or high-fluoride oral conditions;
- local acidification in oxygen-starved crevices;
- combined fretting, wear and corrosion;
- galvanic coupling with unsuitable dissimilar metals;
- cathodic hydrogen charging or improper electrochemical treatment;
- strong reducing acids;
- hot concentrated salts or unusual disinfection chemicals;
- areas containing particles, residues or surface damage;
- new uses lacking device-level corrosion and biological validation.
Engineering caution: Biocompatibility and body-fluid corrosion performance are not determined by grade alone. Roughness, cleanliness, micromotion, wear, crevices, dissimilar metals, fluoride exposure and sterilization residues can affect the final device.
Typical Production Process for ASTM F67 Grade 3 Titanium Bar
- Raw-material selection and charge preparation: Select qualified high-purity sponge and strictly controlled clean revert, closely controlling O, Fe, N, C, H and residuals.
- Electrode preparation: Homogenize, compact and weld a consumable electrode while avoiding iron particles, oil, moisture and foreign contamination.
- Vacuum melting and ingot production: VAR or another qualified vacuum route is commonly used. ASTM F67 specifies finished-material requirements; special melt count or raw-material restrictions must be stated in the order.
- Ingot conditioning and breakdown: Crop unsuitable ends, remove surface defects, and forge or roll to break down the cast structure.
- Hot processing to bar: Forge or roll at controlled temperature, managing grain size, equiaxed alpha structure, dimensions, oxidation and surface quality.
- Annealing and surface conditioning: Apply the qualified anneal, remove scale and alpha case, and control hydrogen pickup and iron contamination.
- Straightening and finishing: Turn, peel, centerless grind or polish to the ordered diameter, tolerance, straightness and roughness.
- Cleaning: Use validated mechanical or chemical cleaning to prevent oil, abrasive, iron and pickling residues. Final implant cleaning remains the device manufacturer responsibility.
- Inspection: Verify chemistry, tensile properties, dimensions, surface, straightness and appearance. Ultrasonic testing, grain size or microstructure must be ordered when required.
- Identification, packaging and traceability: Maintain heat, lot, bar and report correspondence and use clean protective packaging to prevent scratches and cross-contamination.
Manufacturing and inspection note: ASTM F67 specifies material requirements, but special melt count, ultrasonic class, microstructure, grain size, tight straightness, ground surface, clean packaging, EN 10204 3.1 documentation and third-party inspection must be confirmed in the purchase order.